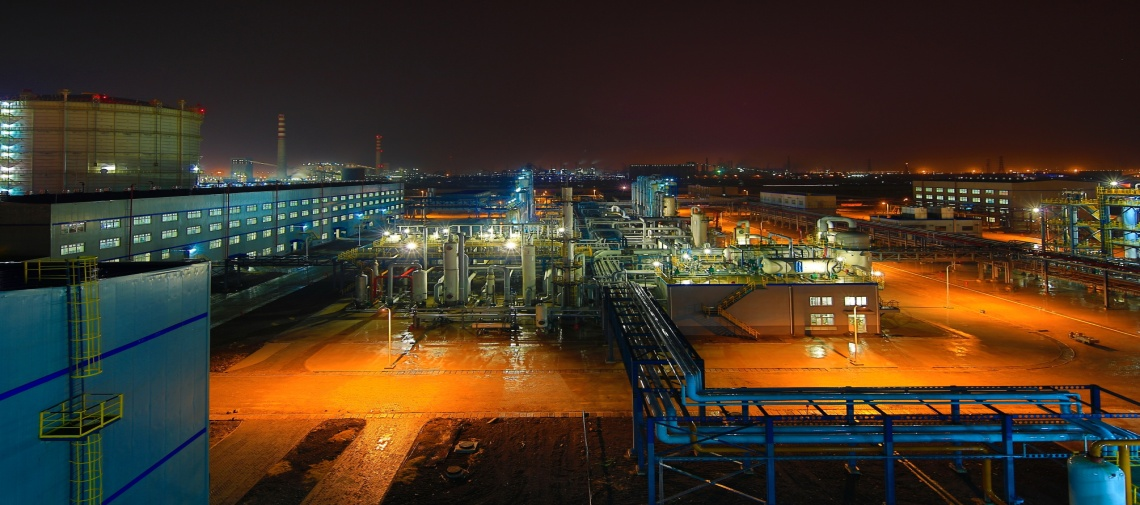
SWCHEM provides technology for producing SNG/CNG/LNG from coke oven gas (COG), with the products obtained through coke oven gas purification, methanation and cryogenic separation.
Based on the composition characteristics of coke oven gas and its existing R&D achievements in methanation catalysts, SWCHEM has developed proprietary process schemes and dedicated methanation catalysts for converting COG to SNG and CNG/LNG. The CNJ-5a dedicated methanation catalyst for COG-to-synthetic-natural-gas applications features high-temperature resistance, high activity, high selectivity, strong hydrocarbon conversion capability and oxygen removal capability.
A fiber-bed demisting and dust-removal process combined with atomized spray washing efficiently removes tar, dust and naphthalene. The equipment features low pressure drop, requires no standby unit, and has an internal service life of at least 10 years. Compared with conventional processes, it can significantly reduce regeneration steam and auxiliary material consumption.
A multi-stage compressor train is adopted with interstage low-temperature purification, together with pressurized naphthalene and oil removal, to achieve deep impurity removal and ensure long-term stable operation of downstream systems.
For high-oxygen operating conditions, the hydrodesulfurization unit adopts quench temperature control and a low-light-off-temperature pre-reforming catalyst to effectively avoid temperature runaway. Heat-integrated energy-saving process design and the elimination of a fired furnace further improve plant safety and energy efficiency.
SWCHEM has proprietary external heat-removal recycle methanation and once-through non-recycle methanation processes, supported by in-house catalysts and extensive industrial references. The technology can efficiently convert CO/CO₂ and crack heavy hydrocarbons and benzene. Both hot-gas recycle and non-recycle schemes can significantly reduce electricity, steam and cooling-water consumption.
The LNG unit adopts a process combining precooling, mixed-refrigerant two-stage separation with three-stage throttling, and nitrogen-cycle refrigeration, together with multi-effect rectification and lithium-bromide waste-heat utilization. The process provides high refrigeration efficiency, low overall energy consumption and stable product specifications, and can flexibly produce SNG, CNG and LNG.
All valuable components in coke oven gas are utilized, with no off-gas discharge. The process can also be integrated with mature ammonia synthesis technology to efficiently utilize cryogenically separated hydrogen and nitrogen streams and improve overall project returns.
Plant capacity can be customized according to project gas flow and production requirements, supporting multiple product routes such as pipeline gas for civil use, CNG filling and LNG sales.
SWCHEM provides:
Click outside to close / Scroll to zoom