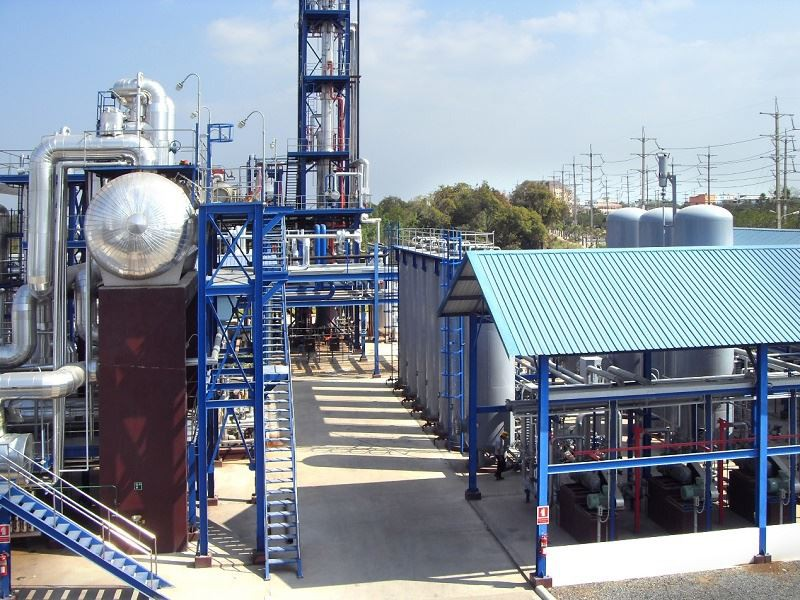
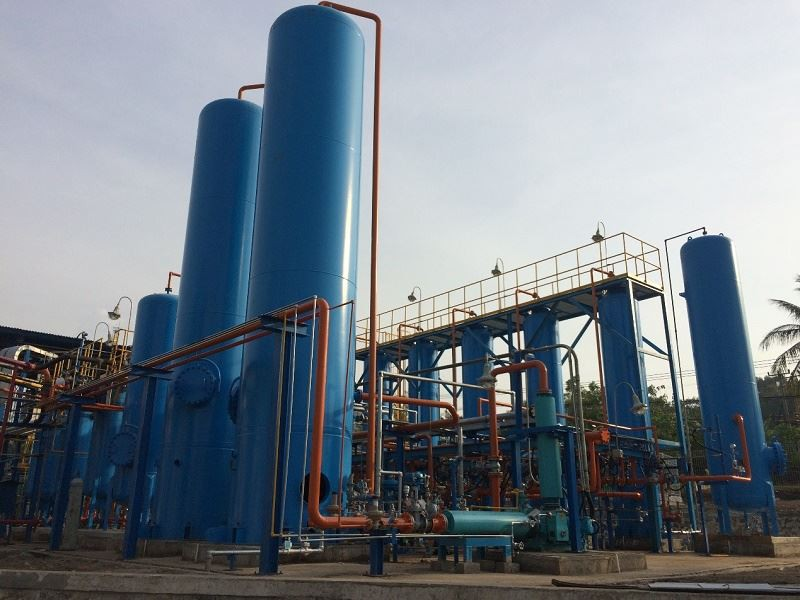
SWCHEM’s natural gas purification technology is used to remove C₂ and heavier hydrocarbon components from natural gas by utilizing the different adsorption capacities of adsorbents for various gas components under different pressure conditions.
During adsorption at elevated pressure, C₂+ hydrocarbon components are selectively adsorbed by the adsorbent, while the unadsorbed gas passes through the adsorber and is collected as purified product gas.
This technology is suitable for natural gas purification and upgrading where removal of heavier hydrocarbons is required
The natural gas purification process is based on selective adsorption and pressure swing regeneration.
At higher pressure, C₂ and heavier hydrocarbon components are adsorbed on the adsorbent bed, while the unadsorbed gas leaves the adsorber as purified gas.
During depressurization, the adsorbed impurity components are desorbed from the adsorbent, allowing the adsorbent to be regenerated and reused in the next cycle.
Typically, at least four adsorbers are required for cyclic operation to ensure continuous output of purified gas.
Applicable feed gases include:
| Item | Data |
|---|---|
| Pressure | 0.3–2.0 MPa(g) |
| Temperature | Ambient temperature |
| Item | Data |
|---|---|
| Product | Purified natural gas |
| C₂ content | ≤ 100 ppm |
| C³ content | ≤ 30 ppm |
| CH₄ recovery | 70-90% |
| System pressure drop, ΔP | 0.10 MPa |
| Temperature | Ambient temperature |
Note: CH₄ recovery depends on feed gas composition, feed pressure and required purified gas specifications.
The purification units are controlled by dedicated controllers and instruments. Depending on the unit scale, automation level and customer control requirements, a DCS control system consistent with the customer’s main plant may be used, or a standalone PLC control system may be selected
In addition to conventional PSA sequence control, loop control and other control functions, SWCHEM also provides specialized control strategies for fully automatic load adjustment, fault diagnosis and fault isolation.
The system can support adaptive optimization, self-diagnosis and fault isolation, improving operational flexibility and helping ensure long-term, stable and safe operation of the unit.
SWCHEM provides:
Click outside to close / Scroll to zoom